Sector Specialty
High-Strength Effluent & ZLD Engineering for Sugar & Distillery
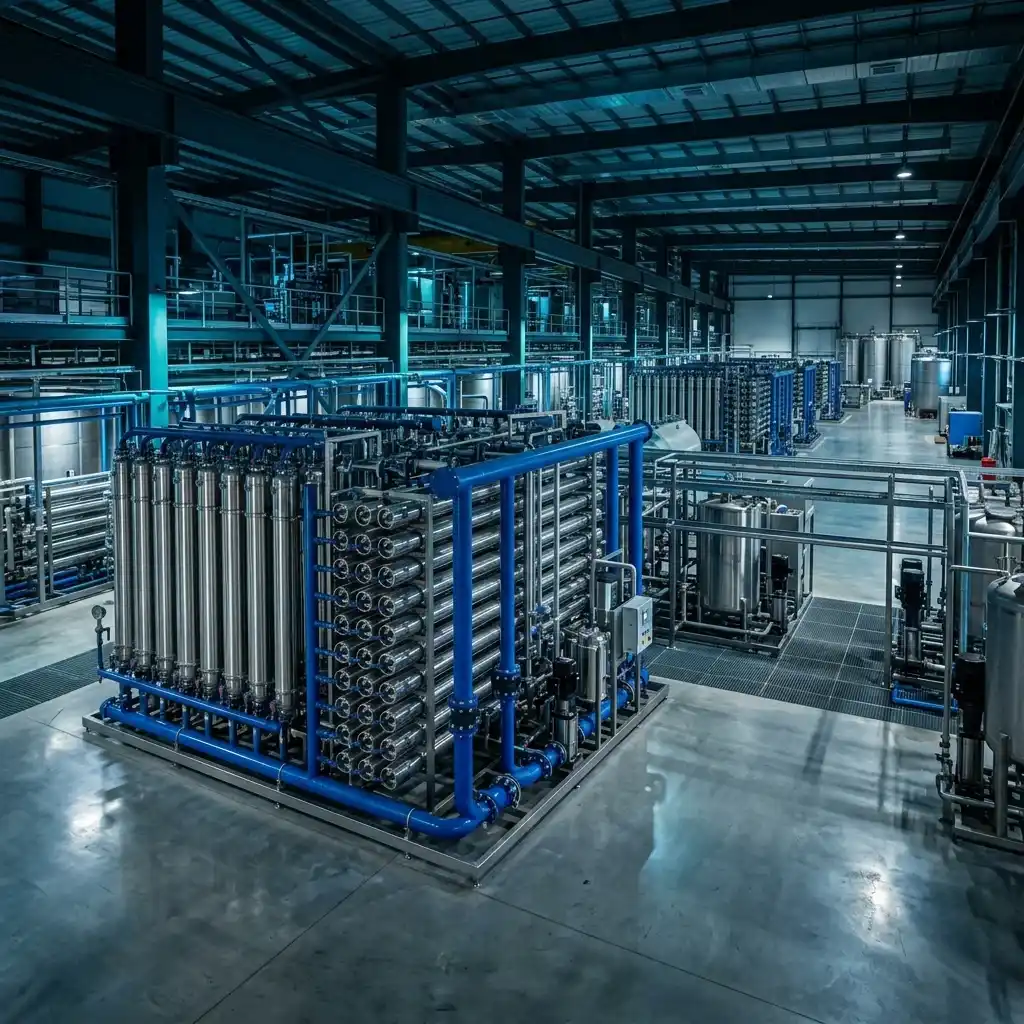
Sugar mills and molasses-based distilleries generate immense volumes of highly complex, organically dense effluents like spent wash and process condensate. We engineer robust biomethanation, evaporation, and condensate polishing systems to achieve strict Zero Liquid Discharge (ZLD) mandates while recovering valuable biogas and high-purity process water.
< 1.3 µS
Conductivity @ 25°C
< 10 CFU
Microbial Limit / 100ml
DQ/IQ/OQ
Validation & PQ Protocols
100%
ZLD Process Recovery
Problem Solving
Distillery Challenges vs. Hydro Engineered Solutions
How our specialized pharmaceutical engineering eliminates persistent operational and compliance bottlenecks.
- Distillery Challenge #1
Extreme COD Spent Wash
Molasses-based distilleries produce dark, acidic spent wash with catastrophic Chemical Oxygen Demand (COD) levels often exceeding 100,000 mg/L. This effluent instantly destroys conventional biological ETPs and causes severe environmental damage if mishandled.
- HydRO Engineering Solution
Biomethanation & MEE Concentration
Deployment of high-rate Anaerobic Digesters to convert heavy organic loads into valuable biogas (methane) for boiler fuel. The anaerobically treated effluent is then processed through Multi-Effect Evaporators (MEE) to concentrate the remaining spent wash into a thick slop suitable for bio-composting or incineration in slop-fired boilers.
- Distillery Challenge #2
Contaminated Evaporator Condensate
Evaporating massive volumes of sugar juice and spent wash generates large amounts of hot condensate. This water is contaminated with volatile organic compounds (VOCs) and exhibits low pH, rendering it highly corrosive and unfit for boiler or cooling tower make-up.
- HydRO Engineering Solution
Advanced Condensate Polishing Units (CPU)
Engineering specialized CPU plants utilizing multi-stage biological reactors, activated carbon filtration, and temperature-resistant RO/UF membranes. These systems specifically strip volatile organics from hot condensate, recovering up to 90% of the water for immediate reuse in high-pressure boilers and cooling networks.
- Distillery Challenge #3
Recalcitrant Color (Melanoidins)
Distillery effluents are saturated with melanoidins—dark brown, polymerized pigment structures formed during sugar processing. These compounds are highly resistant to standard biological degradation and severely block light penetration in aquatic ecosystems.
- HydRO Engineering Solution