Our Products
Chemicals & Consumables
Membranes & Filters

Dosing & Treatment Chemicals
Resins, Media & Activated Carbon
- Product Datasheet
Download complete technical specifications, P&ID layout, and GA drawing guidelines for our Reverse Osmosis (RO) Plants.
Need Expert Advice?
Speak directly with our chief process engineer for raw water feasibility & customized sizing.
- +91 99251 54844
- sales@hydrofiltsep.com
Chemical & Consumables
Membranes & Filters
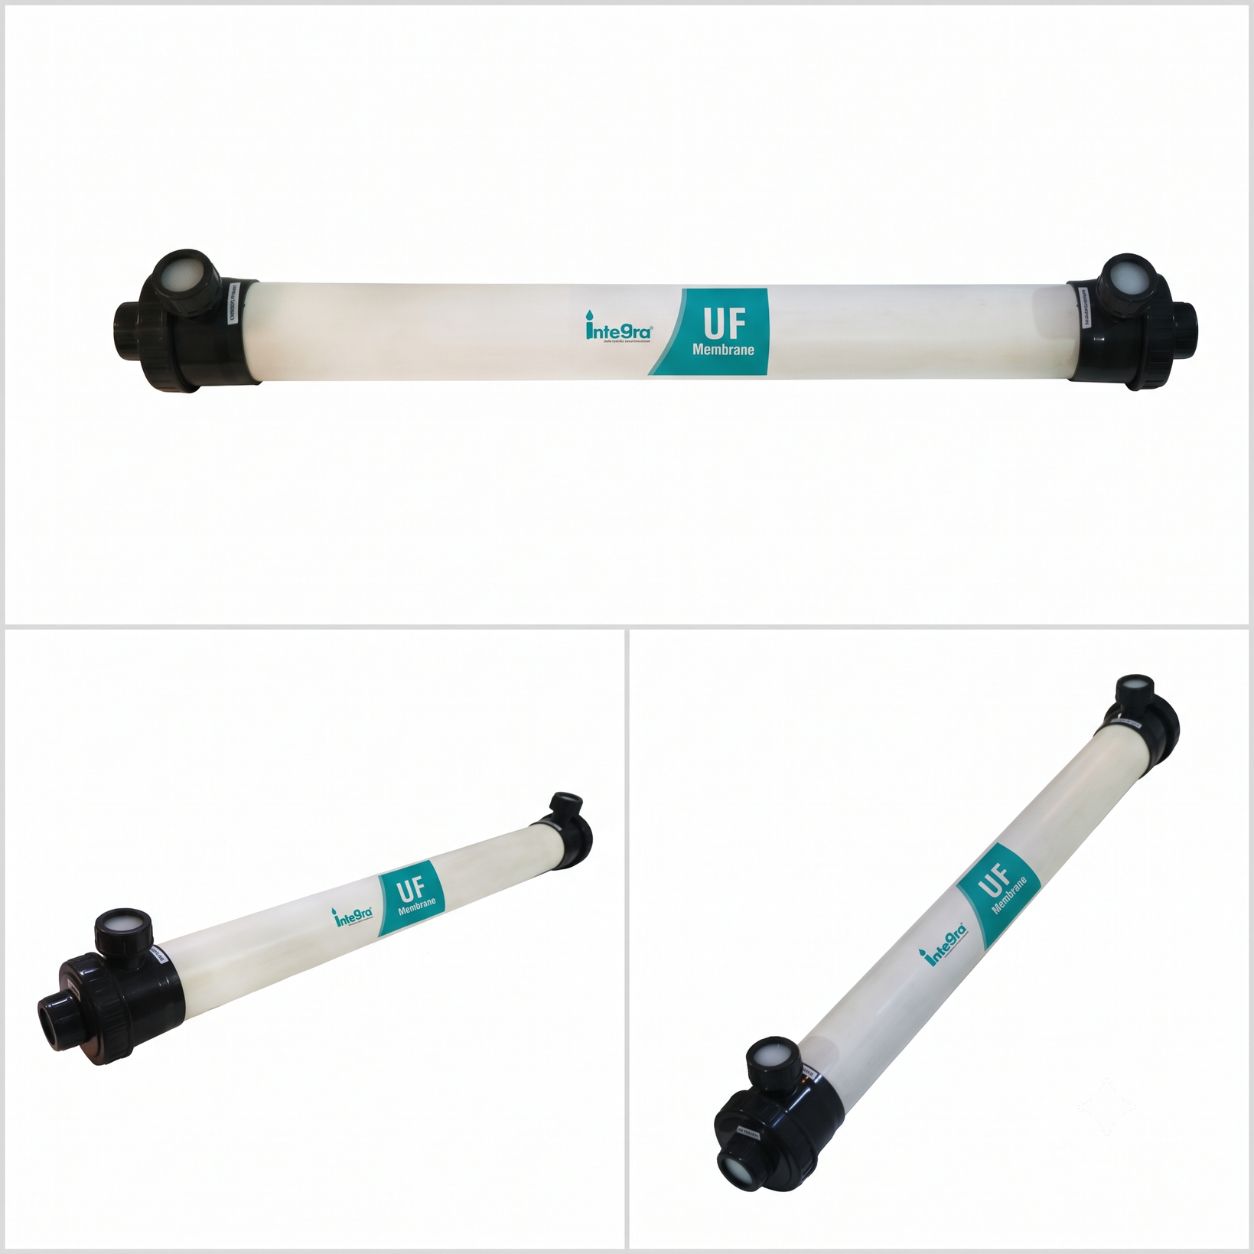
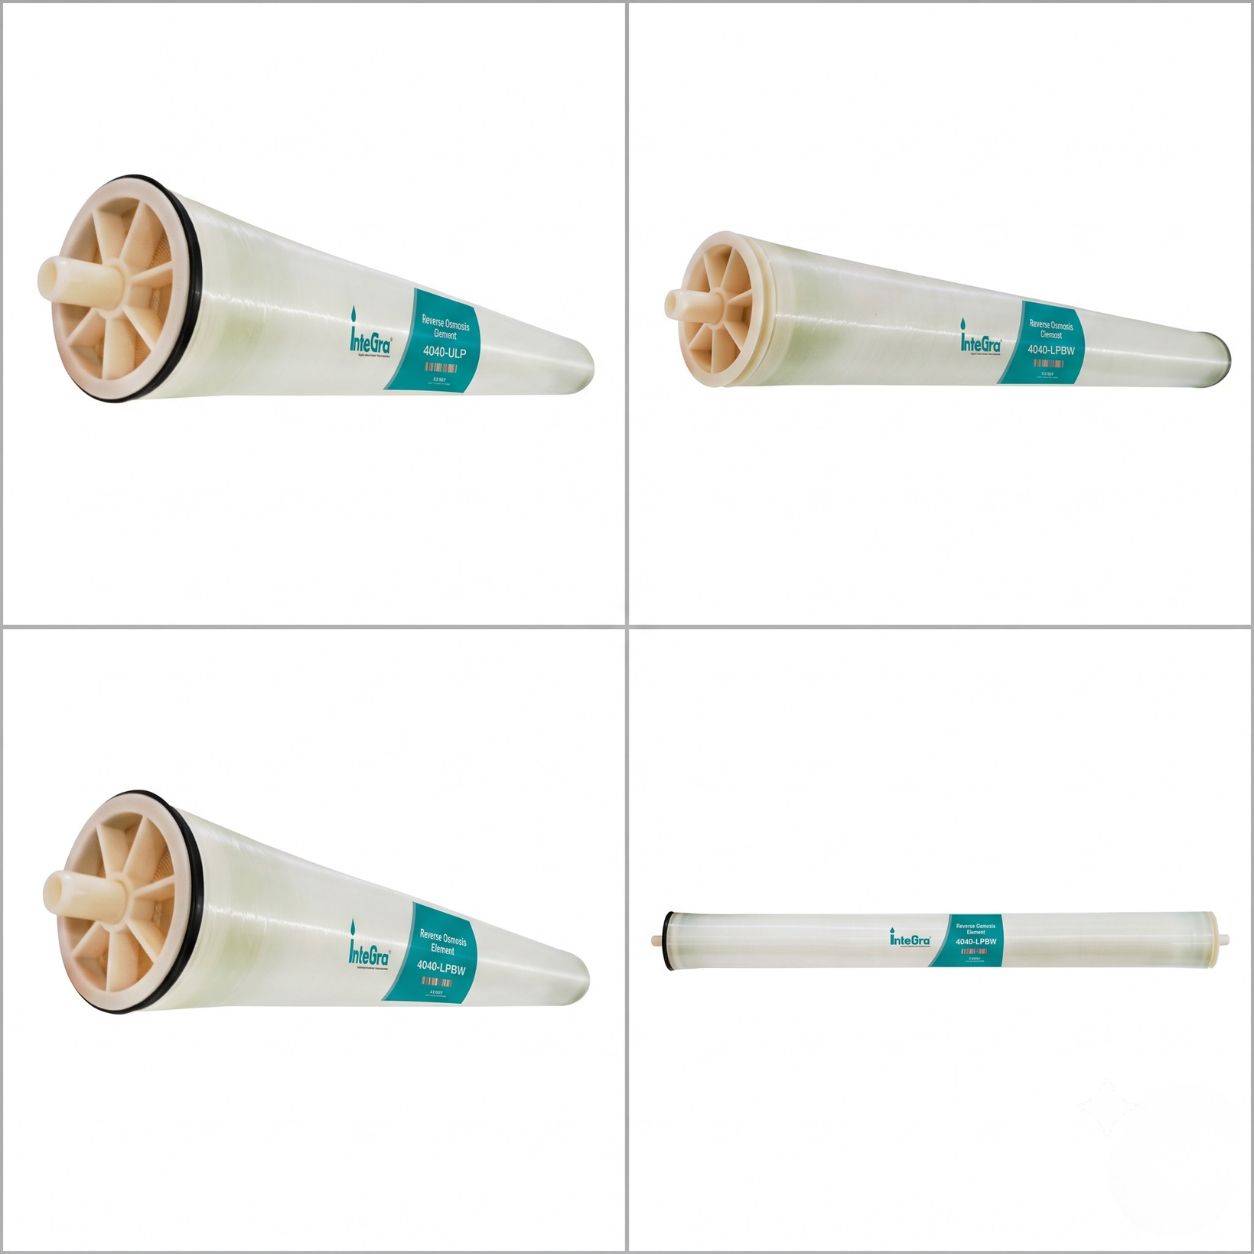
Engineered for harsh industrial and commercial water conditions, our Reverse Osmosis (RO) Plants remove up to 99% of dissolved solids, organics, pyrogens, and colloidal matter. Built with high-grade SS304/316 skids, top-tier TFC membranes, energy recovery systems, and automated PLC/SCADA controls.
Capacity Range
500 – 50,000 LPH
TDS Rejection
Up to 99.2%
Water Recovery
75% – 85%
Automation
PLC / SCADA HMI
Engineering & System Overview
Industrial Reverse Osmosis is a cross-flow membrane separation process that utilizes high-pressure pumps to overcome osmotic pressure, forcing water through semi-permeable spiral wound membranes. Contaminants, dissolved salts, heavy metals, and silica are rejected into the brine stream while ultra-clean permeate is delivered for process or utility use.
At Hydro Filtsep Technologies, every RO plant is custom-engineered based on a Comprehensive water test report. We determine the exact flux rate, membrane fouling factor, array configuration (e.g. 2:1 or 3:2 staging), and pre-treatment requirements to prevent scaling, minimize cleaning frequency, and guarantee long membrane life.
Custom Process Sizing
Designed according to raw water chemistry (TDS, Hardness, Silica, SDI) to avoid premature scaling.
Energy-Saving HP Pumps
Equipped with Grundfos / CRI high-efficiency SS vertical multistage pumps with VFD control.
Heavy Duty SS304/316 Skid
Robust structural framework with passivation and vibration dampening for 24/7 continuous operation.
Integrated CIP System
Built-in Cleaning-In-Place piping and tank system for effortless membrane maintenance.
Treatment Process Flow
Our systematic 5-stage purification sequence protects membranes and produces consistent, high-purity permeate:
1
Raw Water Pre-Treatment
Feed water passes through a Sand & Multi-Grade Filter (MGF) to remove suspended solids, followed by an Activated Carbon Filter (ACF) to eliminate free chlorine, odor, and organics.
2
Anti-Scalant Dosing & Micron Cartridge Filtration
Precise chemical dosing prevents calcium/silica precipitation. 5-micron & 1-micron spun polypropylene cartridge filters capture fine particulate matter, achieving an SDI < 3.
3
High Pressure Booster Pumping
High-pressure vertical multistage centrifugal pumps elevate the pressure (12 to 24 bar) to overcome the osmotic pressure across the membrane train.
4
Reverse Osmosis Membrane Separation
Water is separated into high-purity permeate stream (low TDS) and concentrate reject stream using world-class TFC spiral membranes (DOW Filmtec / Hydranautics).
5
Permeate Disinfection & Storage
Treated water undergoes optional UV sterilization or pH buffering before entering SS304/316 storage tanks ready for plant distribution.
Technical Specifications & Parameters
Standard operational specifications for our Industrial RO series. Custom configurations engineered upon request.
| Technical Parameter | Specification & Standard Range |
|---|
Applications & Sectors Served
Our reverse osmosis systems are operating reliably across numerous industrial sectors throughout India:
- Pharmaceutical & API Formulations
- Chemical & Petrochemical Plants
- Power Plants & Boiler Feed Water
- Food & Beverage Processing
- Textile Processing & Dyeing Units
- Automotive Paint Shops & CED Coating
- Hospitals & Dialysis Centers
- Commercial Complexes & Tech Parks
Ready to Build or Upgrade Your Industrial Water Treatment Plant?
Chemical & Consumables
Dosing & Treatment Chemicals
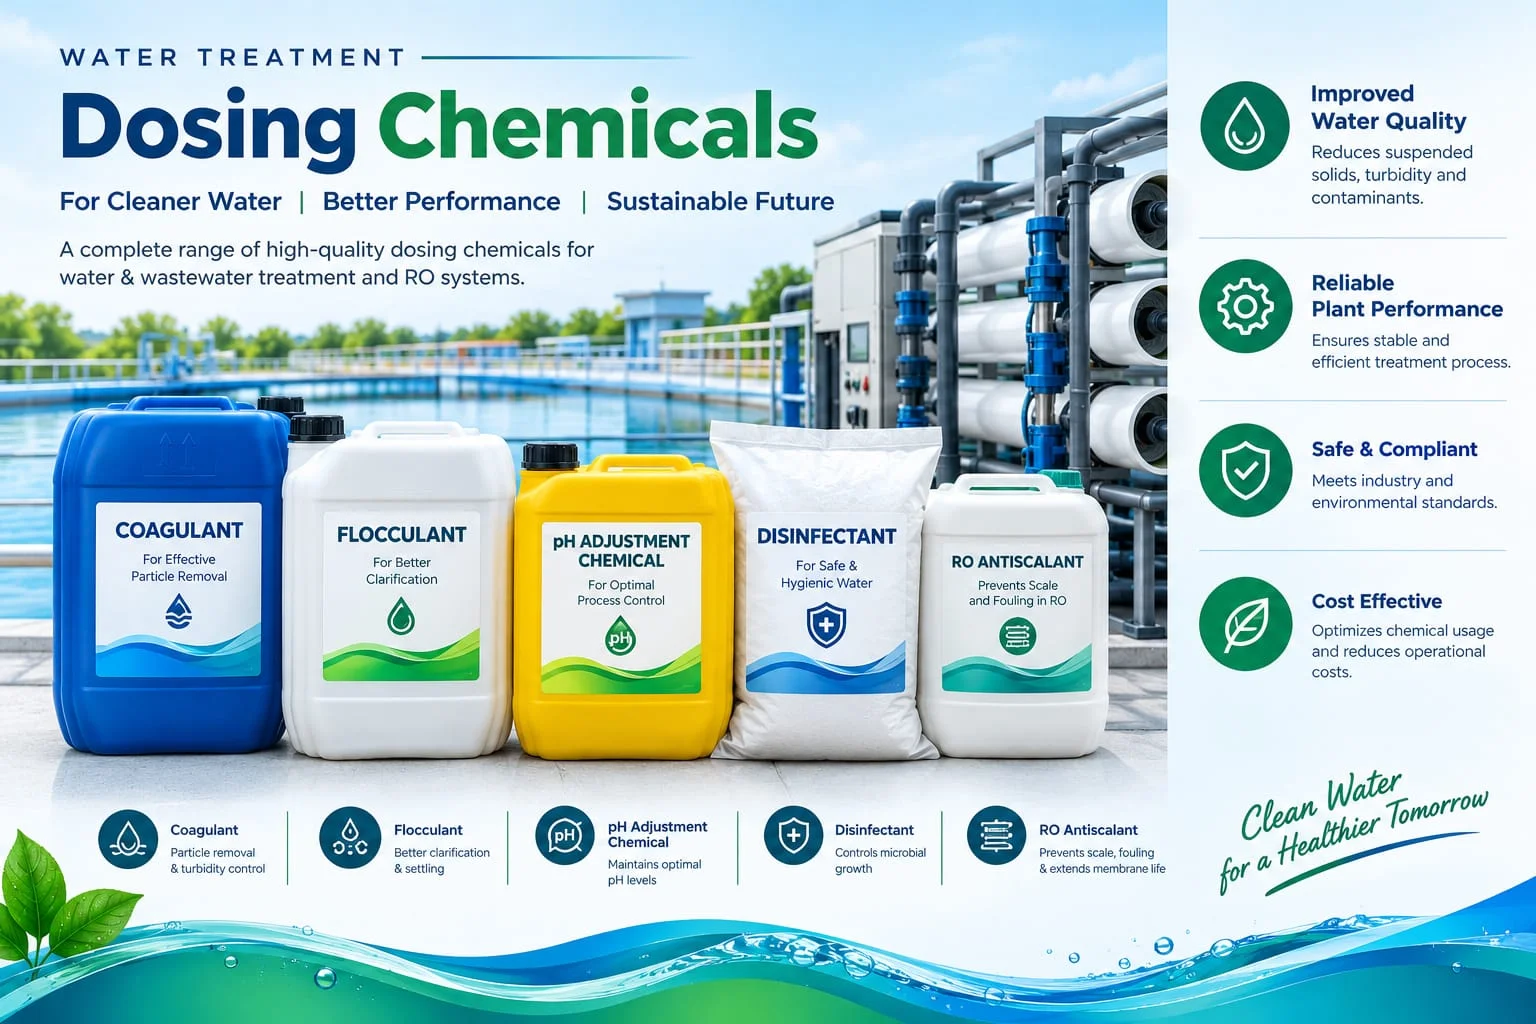
Engineered for harsh industrial and commercial water conditions, our Reverse Osmosis (RO) Plants remove up to 99% of dissolved solids, organics, pyrogens, and colloidal matter. Built with high-grade SS304/316 skids, top-tier TFC membranes, energy recovery systems, and automated PLC/SCADA controls.
Capacity Range
500 – 50,000 LPH
TDS Rejection
Up to 99.2%
Water Recovery
75% – 85%
Automation
PLC / SCADA HMI
Engineering & System Overview
Industrial Reverse Osmosis is a cross-flow membrane separation process that utilizes high-pressure pumps to overcome osmotic pressure, forcing water through semi-permeable spiral wound membranes. Contaminants, dissolved salts, heavy metals, and silica are rejected into the brine stream while ultra-clean permeate is delivered for process or utility use.
At HydRO Filtsep Technologies, every RO plant is custom-engineered based on a comprehensive water test report. We determine the exact flux rate, membrane fouling factor, array configuration (e.g. 2:1 or 3:2 staging), and pre-treatment requirements to prevent scaling, minimize cleaning frequency, and guarantee long membrane life.
Custom Process Sizing
Designed according to raw water chemistry (TDS, Hardness, Silica, SDI) to avoid premature scaling.
Energy-Saving HP Pumps
Equipped with Grundfos / CRI high-efficiency SS vertical multistage pumps with VFD control.
Heavy Duty SS304/316 Skid
Robust structural framework with passivation and vibration dampening for 24/7 continuous operation.
Integrated CIP System
Built-in Cleaning-In-Place piping and tank system for effortless membrane maintenance.
Treatment Process Flow
Our systematic 5-stage purification sequence protects membranes and produces consistent, high-purity permeate:
1
Raw Water Pre-Treatment
Feed water passes through a Sand & Multi-Grade Filter (MGF) to remove suspended solids, followed by an Activated Carbon Filter (ACF) to eliminate free chlorine, odor, and organics.
2
Anti-Scalant Dosing & Micron Cartridge Filtration
Precise chemical dosing prevents calcium/silica precipitation. 5-micron & 1-micron spun polypropylene cartridge filters capture fine particulate matter, achieving an SDI < 3.
3
High Pressure Booster Pumping
High-pressure vertical multistage centrifugal pumps elevate the pressure (12 to 24 bar) to overcome the osmotic pressure across the membrane train.
4
Reverse Osmosis Membrane Separation
Water is separated into high-purity permeate stream (low TDS) and concentrate reject stream using world-class TFC spiral membranes (DOW Filmtec / Hydranautics).
5
Permeate Disinfection & Storage
Treated water undergoes optional UV sterilization or pH buffering before entering SS304/316 storage tanks ready for plant distribution.
Technical Specifications & Parameters
Standard operational specifications for our Industrial RO series. Custom configurations engineered upon request.
| Technical Parameter | Specification & Standard Range |
|---|
Applications & Sectors Served
Our reverse osmosis systems are operating reliably across numerous industrial sectors throughout India:
- Pharmaceutical & API Formulations
- Chemical & Petrochemical Plants
- Power Plants & Boiler Feed Water
- Food & Beverage Processing
- Textile Processing & Dyeing Units
- Automotive Paint Shops & CED Coating
- Hospitals & Dialysis Centers
- Commercial Complexes & Tech Parks
Ready to Build or Upgrade Your Industrial Water Treatment Plant?
Chemical & Consumables
Resins, Media & Activated Carbon
Engineered for harsh industrial and commercial water conditions, our Reverse Osmosis (RO) Plants remove up to 99% of dissolved solids, organics, pyrogens, and colloidal matter. Built with high-grade SS304/316 skids, top-tier TFC membranes, energy recovery systems, and automated PLC/SCADA controls.
Capacity Range
500 – 50,000 LPH
TDS Rejection
Up to 99.2%
Water Recovery
75% – 85%
Automation
PLC / SCADA HMI
Engineering & System Overview
Industrial Reverse Osmosis is a cross-flow membrane separation process that utilizes high-pressure pumps to overcome osmotic pressure, forcing water through semi-permeable spiral wound membranes. Contaminants, dissolved salts, heavy metals, and silica are rejected into the brine stream while ultra-clean permeate is delivered for process or utility use.
At HydRO Filtsep Technologies, every RO plant is custom-engineered based on a comprehensive water test report. We determine the exact flux rate, membrane fouling factor, array configuration (e.g. 2:1 or 3:2 staging), and pre-treatment requirements to prevent scaling, minimize cleaning frequency, and guarantee long membrane life.
Custom Process Sizing
Designed according to raw water chemistry (TDS, Hardness, Silica, SDI) to avoid premature scaling.
Energy-Saving HP Pumps
Equipped with Grundfos / CRI high-efficiency SS vertical multistage pumps with VFD control.
Heavy Duty SS304/316 Skid
Robust structural framework with passivation and vibration dampening for 24/7 continuous operation.
Integrated CIP System
Built-in Cleaning-In-Place piping and tank system for effortless membrane maintenance.
Treatment Process Flow
Our systematic 5-stage purification sequence protects membranes and produces consistent, high-purity permeate:
1
Raw Water Pre-Treatment
Feed water passes through a Sand & Multi-Grade Filter (MGF) to remove suspended solids, followed by an Activated Carbon Filter (ACF) to eliminate free chlorine, odor, and organics.
2
Anti-Scalant Dosing & Micron Cartridge Filtration
Precise chemical dosing prevents calcium/silica precipitation. 5-micron & 1-micron spun polypropylene cartridge filters capture fine particulate matter, achieving an SDI < 3.
3
High Pressure Booster Pumping
High-pressure vertical multistage centrifugal pumps elevate the pressure (12 to 24 bar) to overcome the osmotic pressure across the membrane train.
4
Reverse Osmosis Membrane Separation
Water is separated into high-purity permeate stream (low TDS) and concentrate reject stream using world-class TFC spiral membranes (DOW Filmtec / Hydranautics).
5
Permeate Disinfection & Storage
Treated water undergoes optional UV sterilization or pH buffering before entering SS304/316 storage tanks ready for plant distribution.
Technical Specifications & Parameters
Standard operational specifications for our Industrial RO series. Custom configurations engineered upon request.
| Technical Parameter | Specification & Standard Range |
|---|
Applications & Sectors Served
Our reverse osmosis systems are operating reliably across numerous industrial sectors throughout India:
- Pharmaceutical & API Formulations
- Chemical & Petrochemical Plants
- Power Plants & Boiler Feed Water
- Food & Beverage Processing
- Textile Processing & Dyeing Units
- Automotive Paint Shops & CED Coating
- Hospitals & Dialysis Centers
- Commercial Complexes & Tech Parks