Sector Specialty
High-Purity Water & Zero Discharge Engineering for Pharmaceuticals
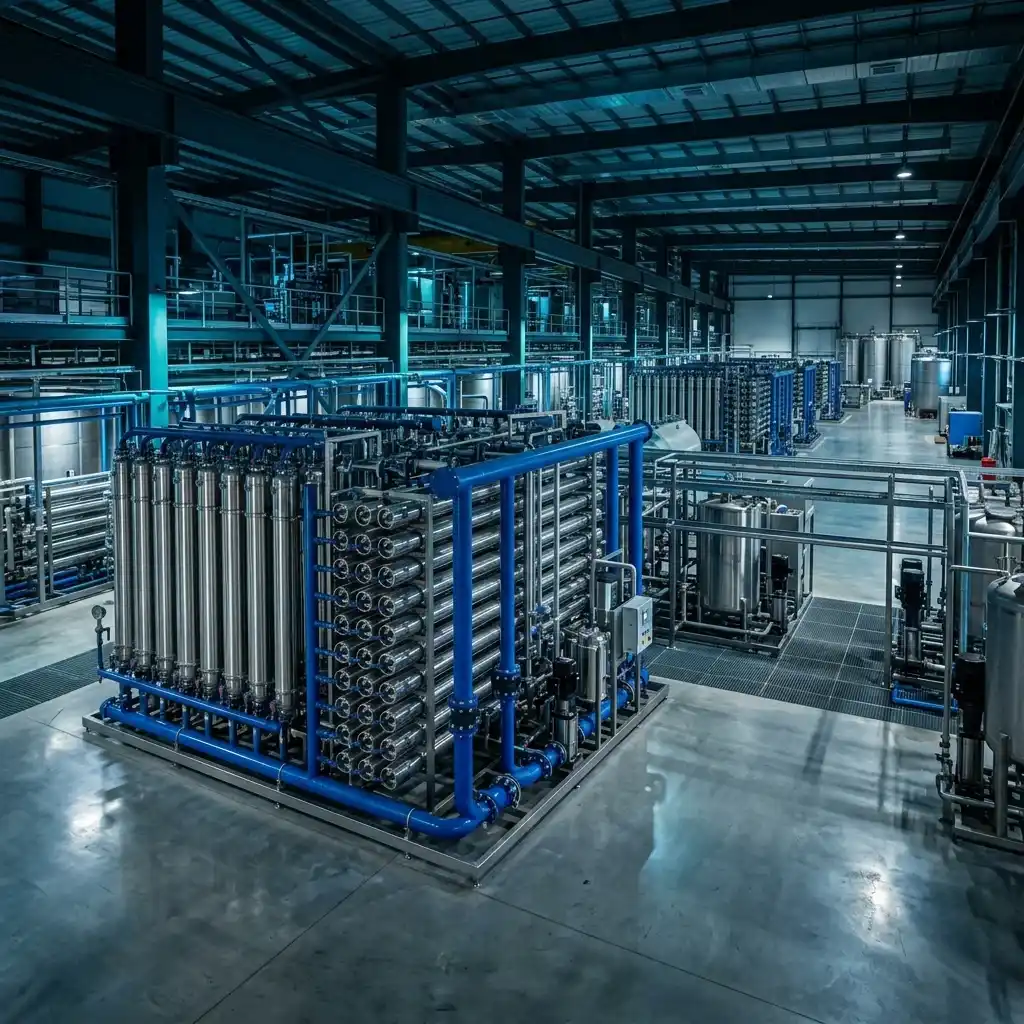
Pharmaceutical and API manufacturing requires uncompromised microbiological purity for formulation, paired with resilient effluent treatment plants capable of degrading toxic, high-COD solvent streams with 100% regulatory compliance.
< 1.3 µS
Conductivity @ 25°C
< 10 CFU
Microbial Limit / 100ml
DQ/IQ/OQ
Validation & PQ Protocols
95%
ZLD Process Recovery
Problem Solving
Pharma Challenges vs. HydRO Engineered Solutions
How our specialized pharmaceutical engineering eliminates persistent operational and compliance bottlenecks.
- Pharma Challenge #1
Biofilm & Bacterial Proliferation
Stagnant zones and rough internal pipe surfaces foster biofilm colonies, causing TOC spikes and failing pharmacopoeia microbial limits.
- HydRO Engineering Solution
Biofilm & Bacterial Proliferation
Stagnant zones and rough internal pipe surfaces foster biofilm colonies, causing TOC spikes and failing pharmacopoeia microbial limits.
- Pharma Challenge #2
Refractory COD & Solvent Shock Loads
Bulk drug syntheses discharge wash water containing volatile solvents and non-biodegradable API residues (COD > 25,000 mg/L) that poison biological ETPs.
- HydRO Engineering Solution
Fenton Oxidation + MBR + ZLD MEE
Multi-stage equalization with catalytic Fenton oxidation, submerged MBR biological polishing, followed by MEE/ATFD evaporators achieving 100% ZLD.
- Pharma Challenge #3
Chemical Carryover from Mixed Beds
Traditional demineralization plants require periodic hazardous acid and alkali regeneration, risking chemical carryover into purified process water.
- HydRO Engineering Solution